Heavy-Duty Industrial Storage Systems
Engineered to comply with international RMI (ANSI MH16.1) and EN 15512 structural standards. Explore our wholesale pallet racking portfolio designed for maximum load capacity, structural stability, and spatial optimization.
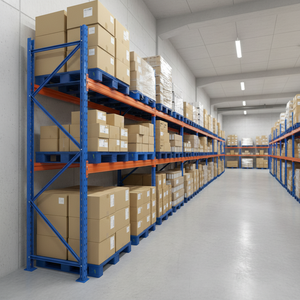
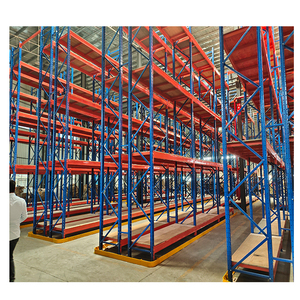
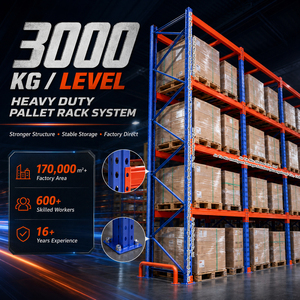
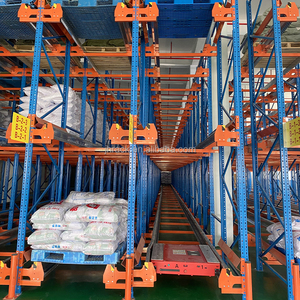
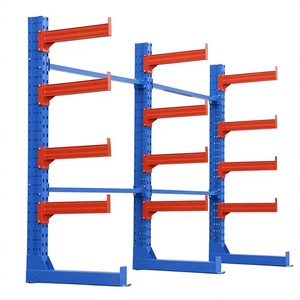
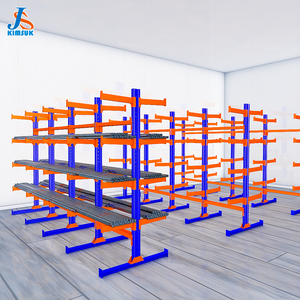
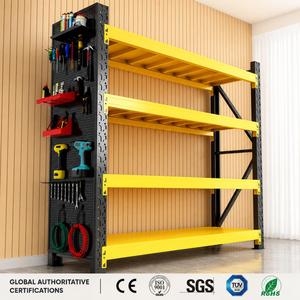
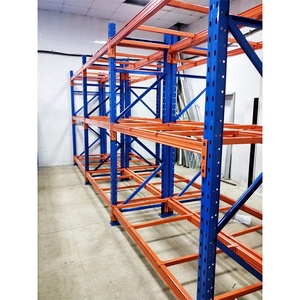
1. Strategic Selection Guide: China Pallet Storage System Wholesale Dynamics
Modern global logistics networks face unprecedented pressure to optimize volumetric warehouse efficiency, lower operating expenses, and ensure complete structural integrity under demanding dynamic loads. As a premier China pallet storage system wholesaler, our manufacturing infrastructure bridges raw metallurgical precision with advanced structural layout engineering. Selecting an industrial-grade pallet racking system requires comprehensive analysis beyond initial procurement costs—it demands an in-depth understanding of steel yield strengths, structural deflection safety factors, seismic engineering parameters, and material handling automation compatibility.
In B2B supply chain procurement, racking infrastructure is not merely static steel shelving; it forms the backbone of operational throughput. Whether engineering a high-turnover selective racking layout for a 3PL distribution center or installing automated radio-shuttle high-density frameworks for cold-chain facilities, working directly with a qualified Chinese structural racking manufacturer provides distinct technical and economic advantages.
Structural Steel Integrity
Exclusively manufactured using high-tensile Q235B and Q355B cold-rolled steel profiles for optimized load-to-weight ratios and dynamic load resistance.
Seismic & Safety Certified
Engineered to withstand zone-specific seismic forces in strict accordance with RMI/ANSI MH16.1, FEM 10.2.02, and EN 15512 standards.
End-to-End OEM/ODM Customization
From CAD layout design and finite element analysis (FEA) modeling to custom powder coating and global container shipping logistics.
2. Technological Trends in Industrial Pallet Racking & Storage Manufacturing
The global warehousing landscape is undergoing a massive shift toward high-density automation and data-driven inventory control. Industrial buyers and logistics architects must evaluate several emerging engineering trends when procuring wholesale pallet storage systems:
A. Shift Toward High-Density Automated Systems (AS/RS & Shuttle Technology)
Floor space costs per square meter continue to escalate globally, driving a transition from traditional manual selective racking to automated systems. Automated Storage and Retrieval Systems (AS/RS) integrated with radio shuttle carts allow warehouses to operate with ultra-narrow aisles (VNA) and achieve floor-to-ceiling volume utilization exceeding 85%. Modern radio shuttle systems support continuous LIFO and FIFO inventory flows while interfacing directly with modern Warehouse Management Software (WMS).
B. Advanced Metallurgy and Cold-Roll Profile Forming
The structural efficacy of industrial pallet racks depends on column upright profile design. Modern manufacturing processes utilize continuous multi-station cold-roll forming lines to create complex upright profiles (e.g., 80mm to 120mm face profiles) with multiple stiffening ribs. Utilizing structural Q355B micro-alloyed steel allows for thinner wall thicknesses while achieving higher ultimate bending moments, reducing deadweight without sacrificing load-bearing safety margins.
C. Sustainable Surface Finishes & Corrosion Resistance
Cold storage facilities (-30°C) and coastal distribution hubs require advanced corrosion protection. The industry has shifted heavily toward automatic multi-stage pre-treatment wash systems followed by electrostatic epoxy-polyester powder coating. For harsh chemical environments or open-air storage yards, hot-dip galvanizing (HDG) conforming to ISO 1461 guarantees multi-decade protection against atmospheric oxidation and moisture condensation.
3. B2B Procurement Trends & Global Wholesale Supply Chain Outlook (2025–2030)
Procurement directors and supply chain managers sourcing wholesale pallet racks from China are navigating a redefined global trading ecosystem. Key trends shaping enterprise-level procurement include:
- Modular & Reconfigurable Design Protocols: Warehouses demand storage hardware that can adapt rapidly to changing SKU dimensions. Boltless teardrop connection systems and 50mm/75mm adjustable beam pitch intervals have become standard requirements for rapid layout reconfiguration.
- Total Cost of Ownership (TCO) Prioritization: Purchasing decisions are shifting from purely initial capital expenditure (CapEx) to TCO. High-quality frame impact protectors, reinforced bottom column boots, and heavy-duty wire decking significantly reduce long-term structural maintenance and rack replacement costs.
- Strict Compliance with Regional Building Codes: Overseas buyers now require factory-direct structural calculation reports verified by local professional engineers (PE). B2B wholesalers must provide finite element structural verification for wind loads, floor slab point loads, and regional seismic acceleration factors.
4. Enterprise Manufacturing Strengths & Quality Assurance Lifecycle
As an established wholesale manufacturer with over two decades of engineering heritage, our facility operates under rigorous quality assurance protocols to deliver dependable, industrial-grade storage solutions. Our core manufacturing competencies include:
- Automated Robotic Welding Infrastructure: All beam connector brackets, column baseplates, and cantilever arms are joined using multi-axis robotic welding cells, ensuring 100% weld penetration, uniform beads, and zero structural inclusions.
- Comprehensive Raw Material Traceability: We source premium steel coils directly from Tier-1 state steel mills. Every production lot undergoes rigorous chemical composition analysis and tensile strength testing, accompanied by full Mill Test Certificates (MTC).
- Stringent Finite Element Analysis (FEA): Our in-house structural engineering team performs rigorous computer-simulated load tests on complex multi-tier layouts to verify buckling limits, beam deflection criteria (L/200), and dynamic impact resistance before fabrication begins.
- Precision Packing & Container Shipping Optimization: Components are bundled using high-density protective strapping, corner guards, and custom wooden cradles designed to maximize 40ft High Cube (40HQ) container space while preventing transit damage during sea transport.
5. Frequently Asked Questions (FAQ) for B2B Procurement
Ready to Optimize Your Warehouse Storage Layout?
Connect directly with our engineering sales team to request custom CAD layout designs, factory-direct wholesale pricing, and structural technical specifications tailored to your supply chain requirements.
Contact Us