Featured Heavy-Duty Industrial Pallet Racking Systems
Engineered for maximum structural integrity, optimized storage density, and seamless integration with automated handling equipment.
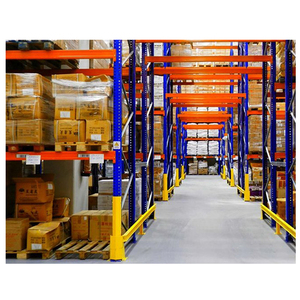
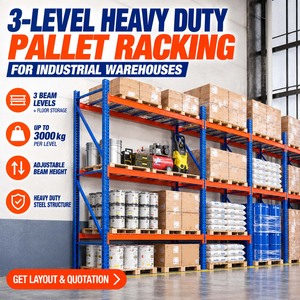
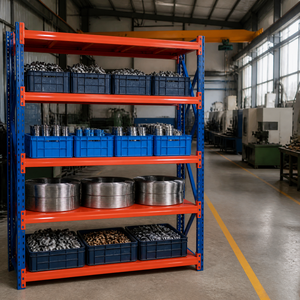
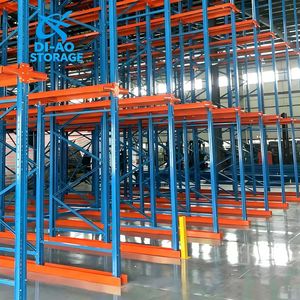
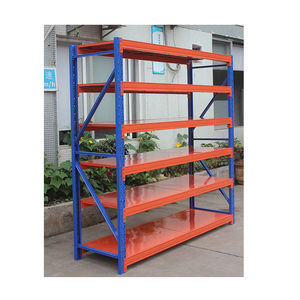
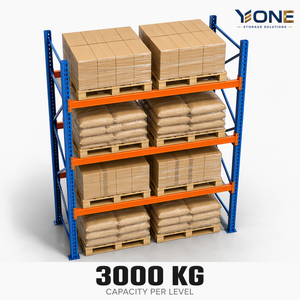
Strategic Manufacturing Dominance: Why Partner with China's Premier Racking Manufacturers
In the contemporary globalized intralogistics ecosystem, industrial warehousing demands storage infrastructure that guarantees absolute structural reliability, volumetric efficiency, and operational scalability. As a leading primary manufacturer and B2B wholesale exporter based in China, our production facility bridges state-of-the-art metallurgical engineering with advanced automated roll-forming technologies. Over two decades of specialized manufacturing experience enable us to engineer pallet racking systems that consistently exceed standard structural criteria established by European (FEM 10.2.02, EN 15512), American (RMI/ANSI MH16.1), and International (ISO 9001, CE) regulatory bodies.
Choosing a tier-one Chinese manufacturer is no longer merely a cost-efficiency initiative; it is a strategic alignment with technical mastery, vertical supply chain integration, and rapid OEM/ODM customization capabilities. Our facilities process thousands of metric tons of prime prime cold-rolled steel coils monthly, ensuring stringent quality assurance from raw material inspection to final electrostatic surface treatment.
Certified Raw Materials
We source exclusively high-grade Q235B and Q355B structural steel from top-tier state steel mills. Yield strengths (fy ≥ 235-355 MPa) and ultimate tensile strengths are rigorously tested to eliminate structural fatigue under dynamic loading.
Automated Precision Milling
Utilizing continuous multi-pass automated roll-forming lines and robotic laser-welding work cells, our upright columns, box beams, and step beams achieve dimensional tolerances within millimeter accuracy.
Advanced Coating Engineering
Components undergo dynamic 6-stage chemical pre-treatment followed by high-adhesion electrostatic epoxy-polyester powder coating (60-80 microns) or ISO 1461 hot-dip galvanizing for coastal/freezer environments.
Engineering Standards & Technical System Architecture
Industrial pallet racking is a complex structural assembly subjected to static, dynamic, and transient shock loads. Understanding beam deflection ratios (L/200 standard), torsional stiffness, column buckling thresholds, and frame bracing geometry is critical when engineering a high-density warehouse storage facility.
Our engineering team performs Finite Element Analysis (FEA) modeling for complex warehouse projects, particularly in high-seismic regions (adhering to seismic zone factors Z=0.4g and above). Below is a comprehensive engineering comparison matrix detailing standard operational parameters across our major heavy-duty racking configurations:
| Racking Architecture | Steel Grade Specs | Max Beam Load (UDL) | Height Capability | Volumetric Density | Access Modality |
|---|---|---|---|---|---|
| Selective Pallet Racking | Q235B / Q355B Cold Rolled | up to 4,500 kg / level | Up to 12.5 meters | Standard (40-50%) | 100% Direct Selective Access |
| Double Deep Racking | Q235B High Tensile Steel | up to 3,200 kg / level | Up to 11.0 meters | High (60-65%) | 50% Direct / Pantograph Reach |
| Very Narrow Aisle (VNA) | Q355B Structural Grade | up to 4,000 kg / level | Up to 18.0 meters | Very High (70-80%) | 100% Direct / Guided Turret Truck |
| Drive-In / Drive-Through | Q235B Heavy Gauge Profile | up to 1,500 kg / pallet | Up to 10.0 meters | Ultra-High (75-85%) | LIFO / FIFO Lane-Based Access |
| Radio Shuttle Racking | Q355B + Alloy Guide Rail | up to 2,000 kg / shuttle | Up to 22.0 meters | Maximum (85-90%) | Automated Semi-FIFO / LIFO |
| AS/RS Automated High-Bay | Q355B Ultra-Precision Frame | up to 3,000 kg / unit load | Up to 40.0 meters | Optimal (90-95%) | Fully Automated Stacker Crane |
All beams are fitted with auto-locking mechanical safety pins engineered to resist vertical impact forces from fork trucks exceeding 1,000 kg displacement thrust, preventing accidental beam dislodgement during operations.
The Future of Industrial Racking Procurement: Key Global Trends
The global warehousing and material handling landscape is undergoing a paradigm shift driven by e-commerce acceleration, land-cost inflation, and labor availability constraints. Modern procurement managers and supply chain directors must evaluate industrial racking investments through the lens of long-term adaptability and technological convergence.
1. The Rapid Shift Toward Automated High-Density Storage (AS/RS & Radio Shuttle)
Conventional low-density selective storage is increasingly being replaced by semi-automated and fully automated high-density storage solutions. Radio shuttle racking systems and AS/RS (Automated Storage and Retrieval Systems) enable distribution centers to utilize vertical air space up to 40 meters while drastically cutting forklift operating costs and thermal loss in cold storage environments.
2. Environmental Sustainability & Green Steel Initiatives
ESG (Environmental, Social, and Governance) compliance is now a mandatory milestone in global enterprise procurement. As a responsible Chinese manufacturer, we are leading the adoption of eco-friendly low-carbon steel processing, closed-loop powder recovery coating lines, and 100% recyclable structural steel components. Lowering embedded carbon without sacrificing yield strength is central to our long-term product roadmap.
3. Dynamic Modular Architecture & Hybrid Storage Configurations
Supply chain demands are more volatile than ever. Modern warehouse designs favor modular, boltless, fully adjustable racking frameworks that allow rapid conversion from selective racking to VNA, or the integration of mezzanine floors above bulk storage zones. Multi-tier racking platforms combined with conveyor integration represent the peak of modern fulfillment center design.
End-to-End Engineering & Global B2B Supply Capability
Our corporate ethos centers on total customer enablement. We do not simply manufacture steel profiles; we deliver complete, turnkey structural logistics solutions tailored to the operational parameters of your specific warehouse facility.
- Comprehensive Architectural CAD & 3D Modeling: Send us your building blueprints, slab load ratings, and pallet specifications. Our engineering team returns fully detailed CAD layout drawings, structural loading calculations, and elevation models within 24 to 48 hours.
- Seismic Mitigation & Custom Baseplate Design: In seismic risk locations, standard baseplates are insufficient. We calculate ground acceleration indices and supply oversized heavy-duty expansion footplates with dual anchor points for max stability.
- Rigorous Quality Control Protocols: Every batch undergoes raw material spectral testing, weld ultrasonic flaw detection, coating thickness micrometer checks, and full-scale beam loading tests (testing to destruction under FEM guidelines).
- Logistics Packaging & Global Containerization: Components are bundle-wrapped in protective plastic film, steel-strapped, and wood-skidded to maximize shipping container space utilization while preventing transit corrosion or scratch damage.
Frequently Asked Questions (FAQ) for Global B2B Procurement
Here are expert answers to critical questions faced by project engineers, procurement officers, and warehouse operations managers when sourcing industrial pallet racking directly from China.
Ready to Optimize Your Warehouse Storage Infrastructure?
Connect directly with our senior structural engineers today. Receive custom CAD layout designs, finite element structural calculations, and competitive factory-direct wholesale pricing within 24 hours.
Get a Quote